GN Solids Control recently completed a significant shipment of solid vacuum pumps and decanter centrifuges to a Middle Eastern oilfield services company. The order included three solid vacuum pumps, one mud cleaner, and one decanter centrifuge, marking another milestone in the company’s expanding presence in the region. This transaction was not an isolated event but part of a broader pattern of repeat business from established clients in the Middle East, where GN has been supplying solid-liquid separation equipment for years.
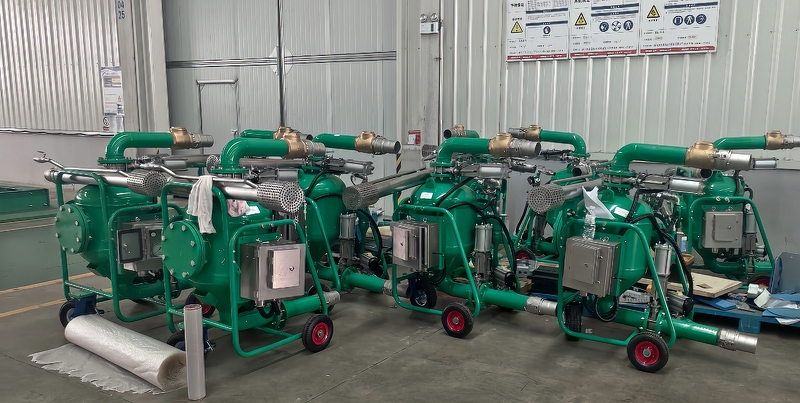
The Middle East presents a demanding environment for drilling operations. High temperatures, abrasive materials, and stringent environmental regulations require equipment that can handle tough conditions while maintaining safety and efficiency. Traditional separation methods often fall short when dealing with high-density materials such as tank bottom sludge, drilling cuttings, and refinery waste. This is where GN’s equipment demonstrates its value. The solid vacuum pump, for instance, uses a purely pneumatic drive system with a Venturi mechanism that generates vacuum levels up to 25 inches of mercury. Because all valves and control components are air-driven, there is no risk of electrical sparks, making the pump suitable for explosive atmospheres commonly found in oil and gas sites. It is specifically designed to transport thick, high-density slurries and solid-liquid mixtures that would clog or damage conventional pumps.
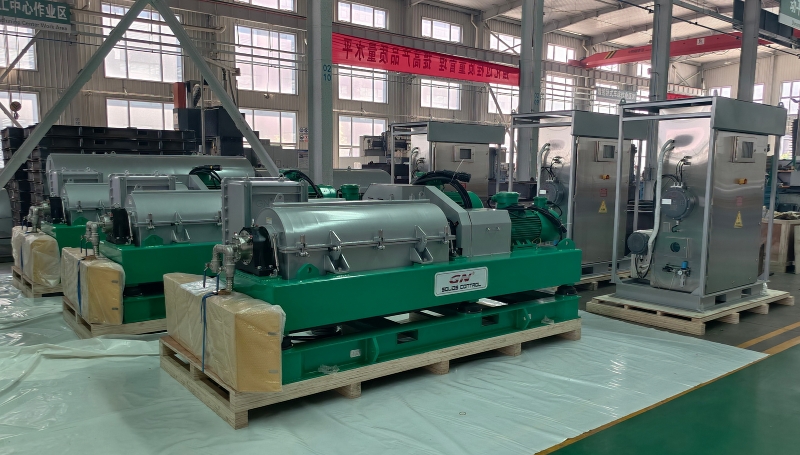
The decanter centrifuges shipped in this batch include both variable-frequency drive models and fully hydraulic versions. The GNLW554ET-VFD, a 22-inch unit, is capable of separating solid particles down to 2-5 microns, making it suitable for large-scale drilling fluid purification and waste volume reduction. The fully hydraulic centrifuges, developed in cooperation with Swiss brands Viscotherm and ROTODIFF, underwent extensive factory testing before shipment. These units offer smooth speed adjustment and reliable heavy-load starting, which are critical in extreme operating conditions. The inclusion of three-phase decanter centrifuges, such as the GNLW364 model, further expands the application range to oil-water-solid separation in oily sludge treatment.
Beyond the primary equipment, the shipment also included customized screw conveyors designed specifically for the customer’s site layout. These conveyors transfer separated solids continuously and are built with wear-resistant spiral blades to extend service life. The removable covers and steel grating options improve both safety and maintenance convenience. This attention to auxiliary components reflects GN’s approach of delivering complete systems rather than standalone machines. The company also supplies mud cleaners, vertical cuttings dryers, and centrifugal pumps compatible with major international brands, allowing clients to standardize their spare parts inventory and reduce operational costs.
The repeat orders from Middle Eastern clients did not happen by chance. GN has invested considerable effort in understanding regional requirements, including explosion-proof standards, material handling characteristics, and environmental compliance. The company’s ability to customize equipment based on specific project needs has been a decisive factor. For example, the 12 drilling cuttings screw conveyors in this order were tailored to the customer’s installation requirements, demonstrating a level of flexibility that large multinational competitors often struggle to match. Additionally, all equipment undergoes rigorous factory testing before delivery, ensuring that units arrive on-site ready for installation and operation. This quality control process minimizes downtime and gives clients confidence in the reliability of the products.
From a broader perspective, this shipment illustrates a shift in how Chinese manufacturers compete internationally. The focus has moved from price advantage to a combination of technology, customization, and after-sales support. GN’s progress in the Middle East is a case in point: by offering equipment that matches or exceeds the performance of established Western brands while providing tailored solutions and responsive service, the company has built lasting relationships with clients who value long-term reliability over initial cost savings. The fact that many orders come from repeat customers indicates that the equipment performs well in real-world conditions, which is the strongest endorsement any industrial supplier can receive.
Looking ahead, the demand for efficient solid-liquid separation and waste management in the Middle East is expected to grow as environmental regulations tighten and operators seek to reduce their ecological footprint. GN’s continued investment in research and development, particularly in areas like oily sludge treatment and three-phase separation, positions the company well to capture additional market share. The successful delivery of this batch of solid vacuum pumps and decanter centrifuges serves as a practical demonstration of the company’s capabilities and reinforces its reputation as a reliable partner for complex separation challenges in the region.