Author Archives: mudcleaner

Two Sets Mud Cleaning System for Trenchless Engineering Company

The trenchless technology industry continues to expand globally as infrastructure demands grow and environmental regulations tighten. Unlike traditional open-cut excavation, methods like Horizontal Directional Drilling (HDD) and Pipe Jacking allow for the installation of pipelines beneath obstacles—such as rivers, highways, and existing urban infrastructure—with minimal surface disruption. However, the success of these methods relies heavily on the management of drilling fluids.

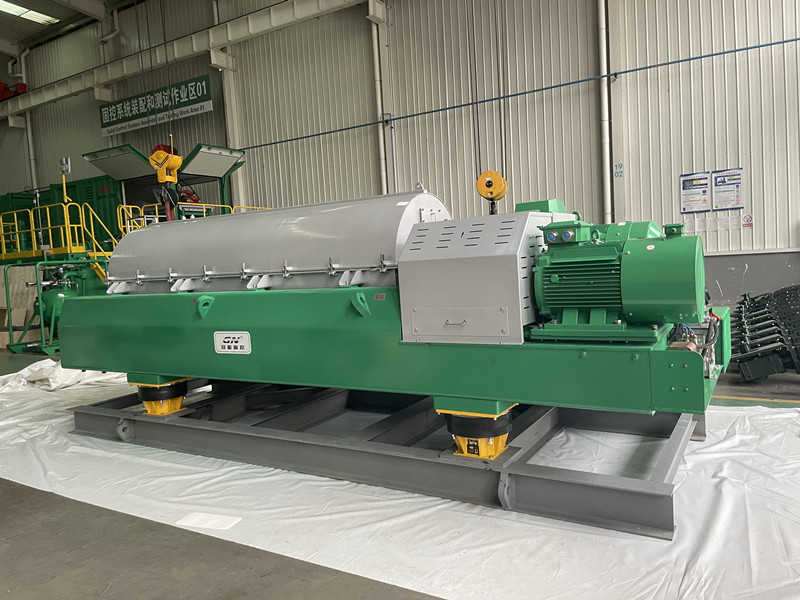
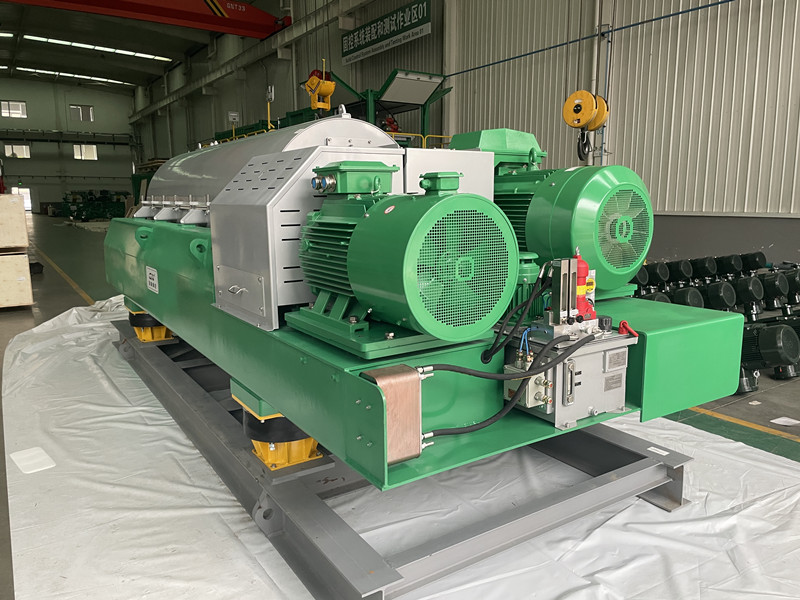
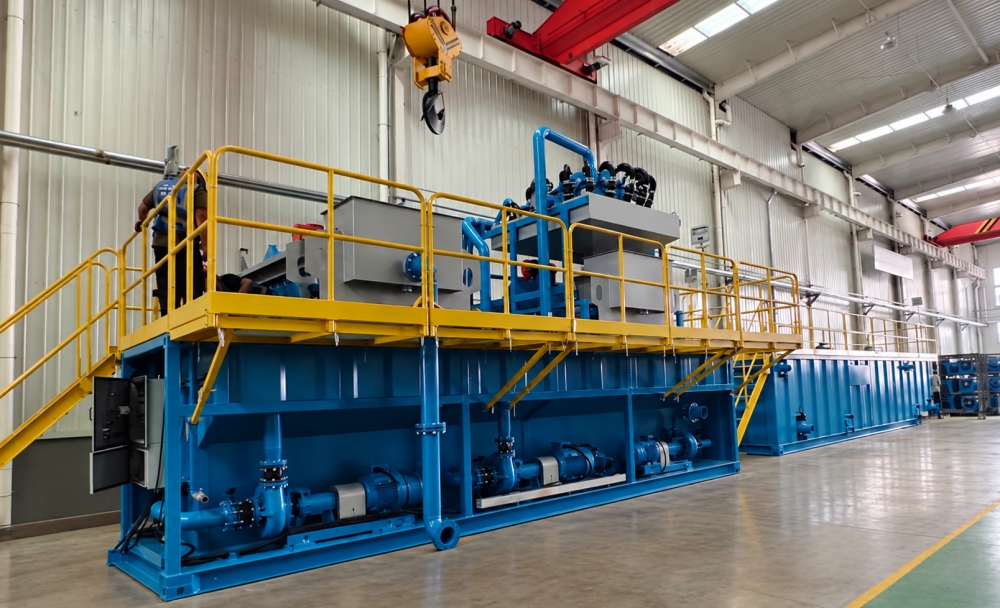
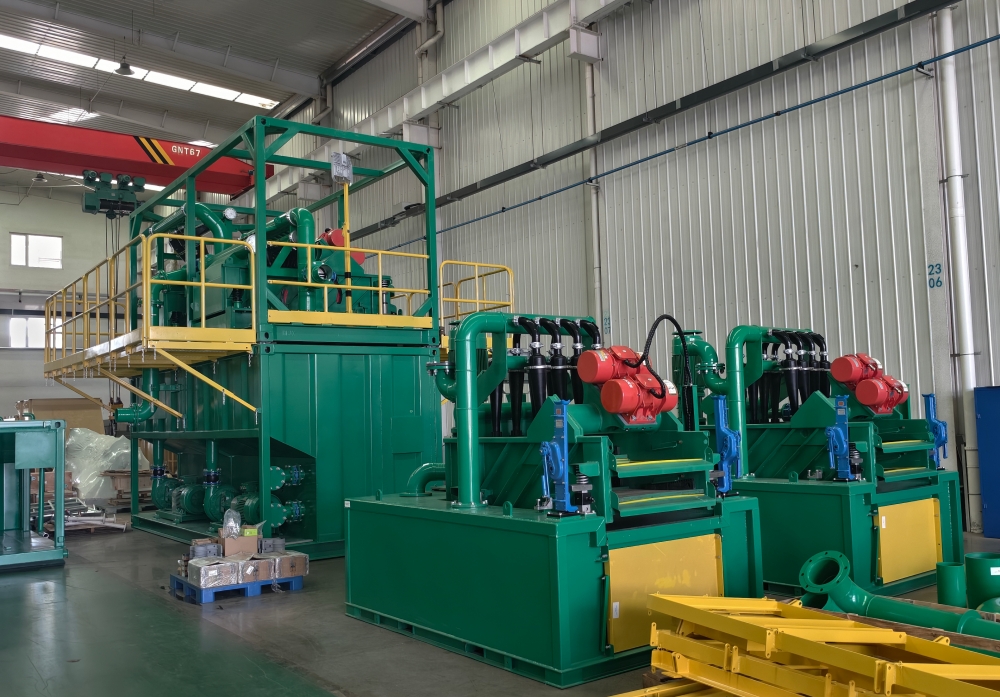
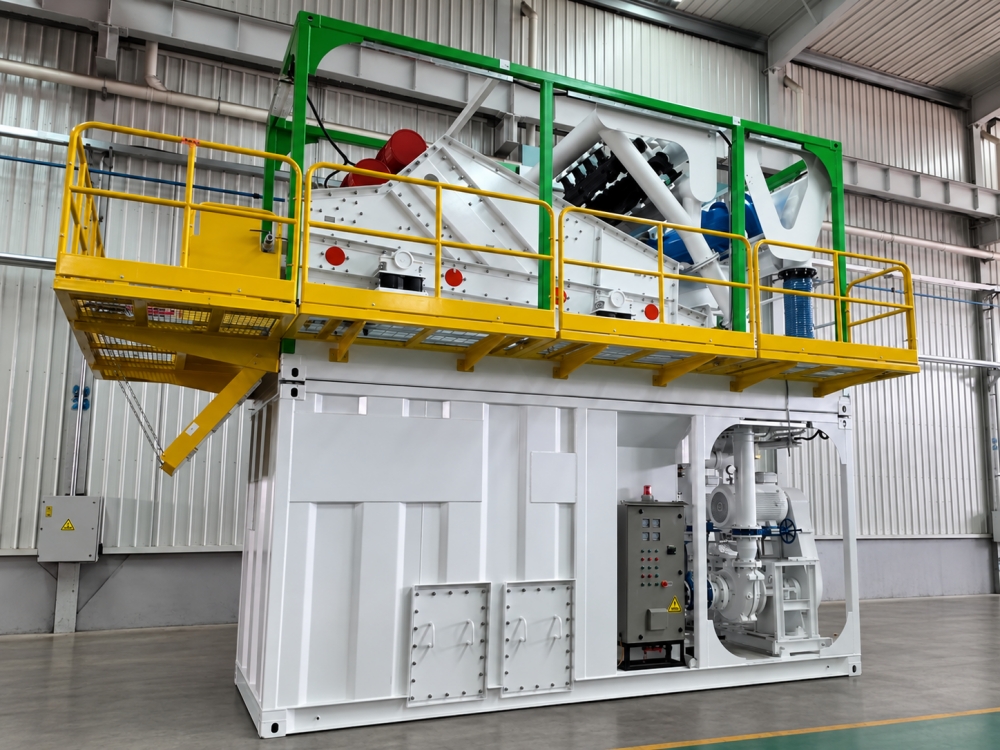
Recently, GN Solids Control successfully manufactured and shipped two distinct non-excavation mud purification systems to a leading trenchless engineering company. This shipment includes one GNMS-1000 Mud Recycling System for HDD projects and one GNTBM-360 Slurry Separation System for pipe jacking operations. These systems represent the cutting edge of solids control technology, designed to maximize fluid recovery, reduce waste disposal costs, and ensure project continuity.
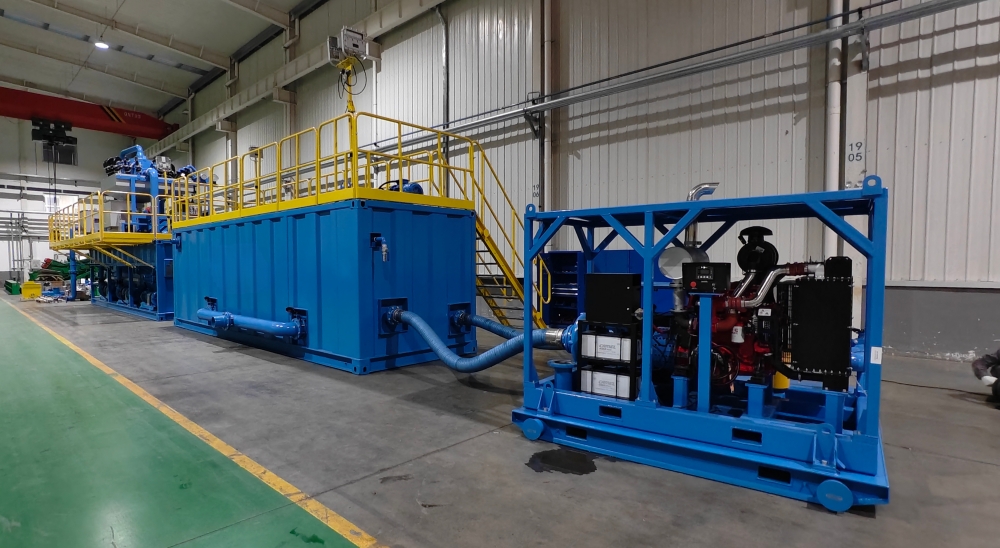
Before diving into the specifics of these two units, it is important to understand why mud management is the “lifeblood” of trenchless construction.

In HDD, the drilling fluid (or “mud”) serves multiple functions: it lubricates the drill bit, stabilizes the borehole, cools the drilling tools, and carries the cuttings back to the surface. Without a high-performance recycling system, the fluid becomes too thick with solids, leading to stuck pipes, borehole collapse, or hydro-lock.

Similarly, in Pipe Jacking and micro-tunneling, a stable slurry front is required to support the tunnel face and transport excavated soil out of the borehole. If the slurry is not properly separated and cleaned, it can lead to reduced advance rates, increased wear on mechanical components, and environmental hazards.

By utilizing advanced separation equipment, contractors can recycle up to 80-90% of their drilling fluid, significantly reducing the need for fresh water and additives while minimizing the volume of waste slurry that must be trucked off-site.

System 1: GNMS-1000 for Horizontal Directional Drilling (HDD)

The first system in this shipment is the GNMS-1000, a high-capacity mud purification system specifically engineered for large-scale HDD crossing projects.

• Capacity: 1,000 Gallons Per Minute (GPM) / 240 Cubic Meters Per Hour (m³/h).

• Primary Separation: A high-G force linear motion shale shaker. This serves as the first stage of defense, removing larger drilled solids (typically >100 microns) from the returning drilling fluid.

• Secondary & Tertiary Separation: A high-efficiency Mud Cleaner. This unit combines a fine-mesh screen shaker with a bank of hydrocyclones (desanders and desilters). It effectively strips away abrasive silts and sands that could damage expensive downhole tools.
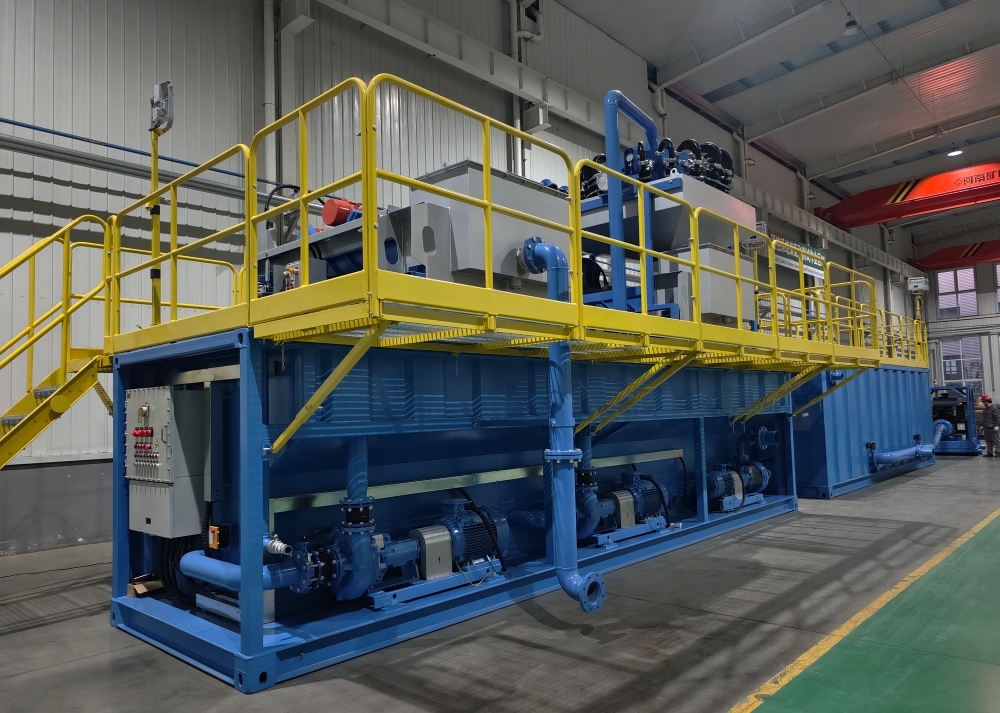
• Mixing System: A Diesel-Driven Mud Mixing Pump. This is a critical feature for remote HDD sites where electrical power may be unreliable or unavailable. The diesel engine ensures continuous operation, allowing operators to precisely blend bentonite or polymers into the clean mud stream to maintain optimal viscosity and gel strength.

For a typical HDD contractor, the GNMS-1000 is ideal for river crossings or long-distance utility installations. The system ensures that the mud properties remain consistent throughout the drilling process. By removing detrimental solids, the GNMS-1000 protects the positive displacement mud motors and drill bits from excessive wear, ultimately saving the contractor thousands of dollars in tool replacement costs.

System 2: GNTBM-360 for Pipe Jacking and TBM Projects

The second system, the GNTBM-360, is designed for a different but equally demanding environment: Pipe Jacking and Slurry Shield Tunneling.

• Capacity: 360 m³/h.

• Vibrating Screen: A robust coarse-screen shaker designed to handle the high volumes of excavated soil and rock slurry generated at the tunnel face.

• Double-Deck Cleaner: Unlike standard systems, the GNTBM-360 utilizes a double-deck cleaning system. The upper deck handles coarse separation, while the lower deck, equipped with desander and desilter cones, performs fine filtration.

• Integrated Tank & Pumps: The system features a compact, integrated tank design with dedicated slurry feeding pumps. This ensures a consistent supply of clean slurry is returned to the jacking machine to maintain face stability.
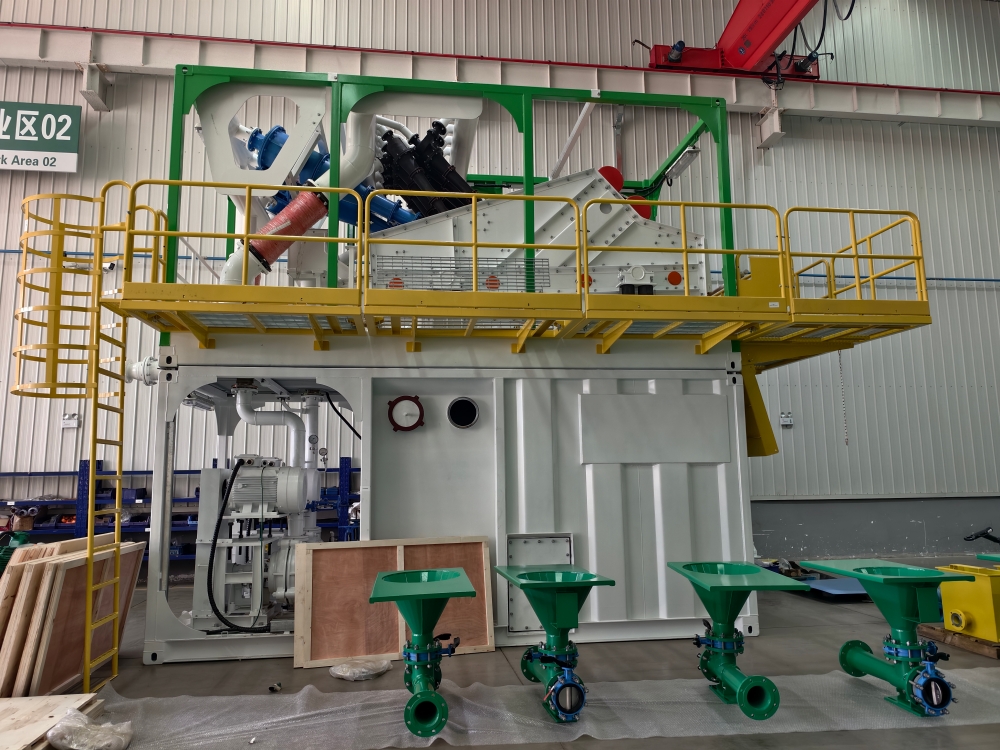
In pipe jacking, the excavation chamber is filled with pressurized slurry. As the cutter head rotates, soil mixes with the slurry and is pumped back to the surface separation plant. The GNTBM-360 excels at rapidly separating these solids. Clean slurry is immediately recirculated back down the pipeline to the tunnel face, while the dewatered spoils can be easily handled by conveyor or excavator. This closed-loop system is vital for urban projects where space is limited and environmental noise/dust must be controlled.

The dispatch of these two systems highlights the versatility of GN’s product line. Whether the client is dealing with the high-flow demands of an HDD rig or the high-density slurry of a micro-tunneling project, GN provides tailored solutions.

1. Durability: Built with abrasion-resistant materials (such as polyurethane hydrocyclones and high-chrome shaker screens) to withstand harsh drilling environments.

2. Mobility: Designed for easy transport between job sites, with compact footprints suitable for congested urban areas.

3. Automation: Features level sensors and automatic starters to ensure safe, continuous operation with minimal manual intervention.

4. Customization: As seen with the diesel-driven pump on the GNMS-1000, GN can customize power sources and configurations to meet specific site requirements.

As cities grow and the need for underground utilities (fiber optics, water, gas) increases, the trenchless industry will continue to move toward larger diameters and longer distances. This evolution demands more sophisticated fluid management.

The integration of high-efficiency mud recycling and slurry separation systems is no longer a luxury—it is a necessity for competitive trenchless contractors. By investing in reliable equipment like the GNMS-1000 and GNTBM-360, engineering companies can ensure they meet project deadlines, stay within environmental compliance, and maximize their return on investment.

GN Solids Control remains committed to supporting the global trenchless community with innovative solids control solutions. From the design phase to after-sales service, we ensure our clients have the tools they need to dig deeper, cross further, and build the infrastructure of tomorrow.
GN Sand Pumps Win Wide Application Across the South American Marke

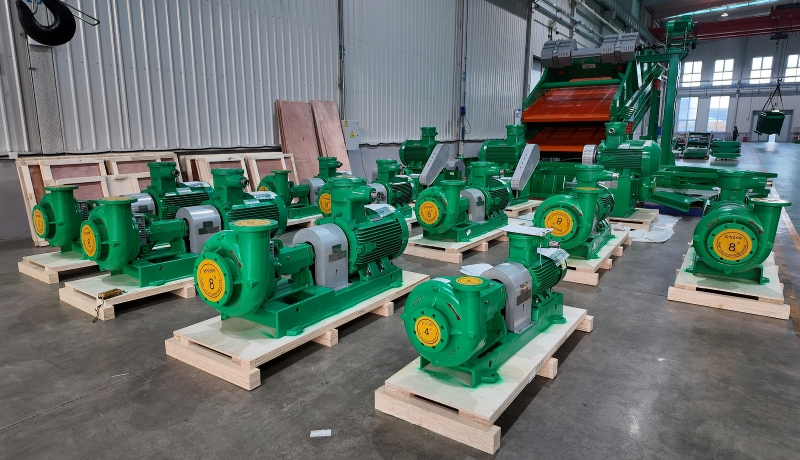
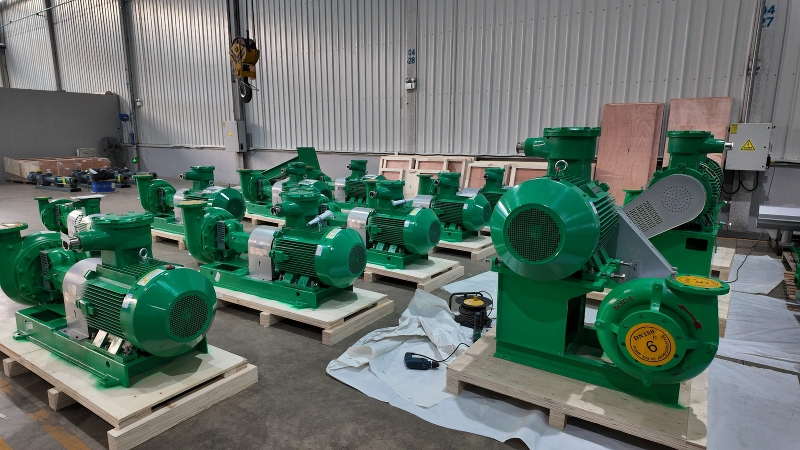
GN Solids Control’s GNSB series centrifugal sand pumps have become a trusted workhorse across the South American market, serving oil & gas drilling, tunneling, piling, and environmental slurry projects from Argentina to Bolivia and beyond.

South American ProjectsSouth American job sites are demanding—remote locations, abrasive drilling mud, high solids content, and mixed voltage standards (50Hz/60Hz). GN sand pumps are built exactly for these conditions:

• Wear-resistant build: casing and impeller made from hard ductile iron alloy, with tungsten carbide mechanical seals for long service life in sandy, corrosive mud.

• Interchangeable spare parts: 100% compatible with major international brands cutting inventory cost for local service teams.

• Open impeller design: lowers axial thrust, extends bearing life, and handles high-viscosity slurry without clogging.

• Flexible models: flow from 35–320 m³/h, power from 7.5–75 kW, 50Hz/60Hz motor options.

• Drilling mud systems: feeding desanders, desilters, and mud cleaners; transfer pump between tanks; charging pump for rig mud pumps.

• Argentina mud recycling: GN 500GPM systems shipped to Argentina use GNSB5×4J sand pumps to drive the GNZY705E mud cleaner, keeping bentonite slurry clean for TBM and piling work.

• Bolivia drilling rigs: sand pumps paired with GNLW452D centrifuges and shale shakers for two rigs, handling abrasive cuttings-laden fluid.

• Wastewater & sandy slurry transfer: GN centrifugal sand pumps also move wastewater with sand/silt for mining and environmental clients.

For South American contractors, the pump is not just a component—it is the circulation heart of the solids control loop. GN sand pumps reduce downtime, simplify maintenance, and keep cones and centrifuges fed at stable pressure. Combined with GN mud cleaners, centrifuges, and screw pumps, they form a complete closed-loop mud system that cuts fluid loss and disposal cost.

With repeated orders from Argentina, Bolivia, and regional oilfield service companies, GN sand pumps are no longer “trial equipment”—they are standard-spec choices. Backed by GN’s API/ISO/ATEX certifications and Americas-side support, the GNSB platform continues to expand across the continent.

From the Andes to the Pampas, GN sand pumps keep the mud moving—reliably, efficiently, and cost-effectively.

GNSP-10B Vacuum Pump Delivered to Mexican Client

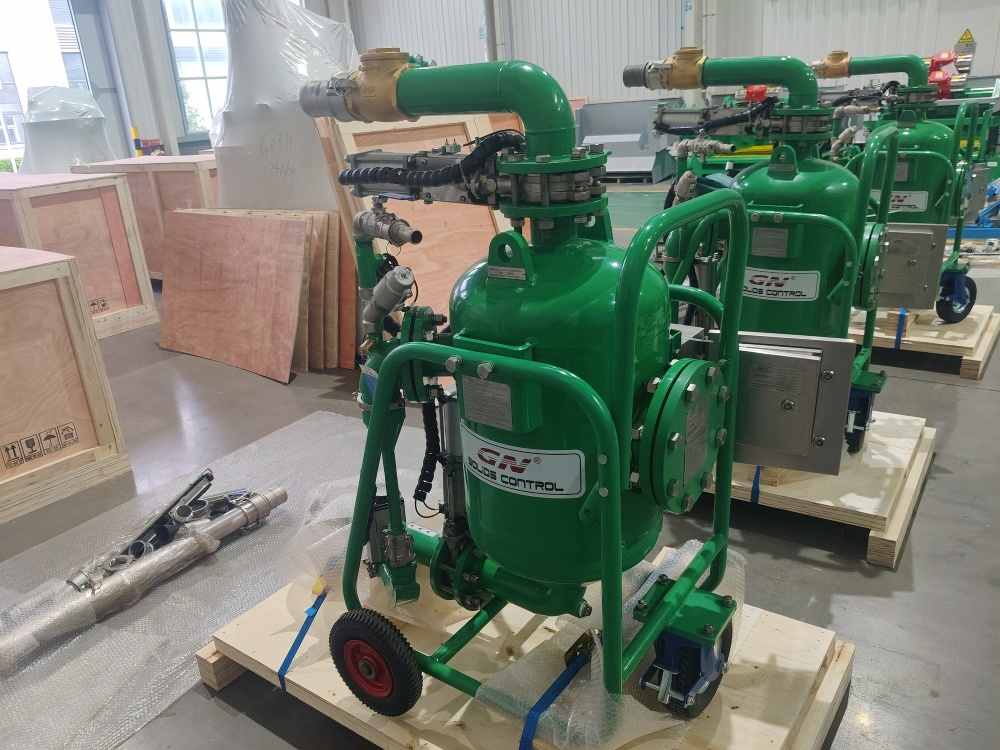
GN Solids Control has completed delivery of its GNSP-10B solid vacuum pump to a client in Mexico. The unit is a 100% pneumatically driven vacuum pump designed for transferring high-solids-content materials, sludge, and powders. This delivery reflects a growing demand in the Mexican industrial market for safe, low-maintenance material handling equipment that can operate in hazardous environments without electrical components.

Traditional electrically driven vacuum systems present inherent risks when handling flammable dusts, sludges, or volatile compounds. Any electrical component—motors, switches, sensors—can serve as an ignition source. The GNSP-10B eliminates this risk entirely by using compressed air as its sole power source. It carries ATEX certification, meeting European and international standards for explosion-proof equipment. For Mexican clients in petroleum, chemical, and mining sectors, this certification is not a luxury; it is a prerequisite for site approval.

The pump also addresses a practical maintenance concern. Unlike rotary vane or liquid ring pumps, the GNSP-10B contains no rotating parts in the traditional sense. It operates on a pneumatic pulse principle, which means fewer wear components, lower failure rates, and longer service intervals. In abrasive conditions—such as transferring mining tailings or gritty sludge—this design advantage translates directly into reduced downtime and lower total cost of ownership.

The GNSP-10B handles up to 10 cubic meters per hour of material. Its 3-inch (89 mm) inlet and outlet diameter strikes a balance between flow capacity and compact physical footprint. The unit measures 1283 mm × 800 mm × 1370 mm and weighs 320 kg, making it manageable for installation in space-constrained workshops or mobile skid configurations.

The pump achieves a vacuum level of 85 kPa (25 inches Hg), sufficient to draw material from distances up to 50 meters. It can pass particles up to 50 mm in diameter and handle materials with solids content as high as 80%. These parameters suit it to applications ranging from drilling cuttings transfer to dry powder conveyance.

Air consumption is rated at 4.3 cubic meters per minute (150 CFM) at a supply pressure of 550–690 kPa (80–100 PSI). Most industrial facilities already operate compressed air systems in this range, so integration typically requires only a connection point and a filtration unit. The pump operates in automatic mode via internal pneumatic logic, cycling between suction and discharge without manual intervention. Quick-release couplings and Barker tube connections simplify pipe hookup during installation.

The client received the GNSP-10B faster than typical lead times for comparable imported equipment. This was not accidental. GN maintains pre-production inventory of core components and complete units for its solid vacuum pump series. When an order arrives, the company skips raw material procurement and machining stages, moving directly to final assembly and testing. This strategy compresses delivery timelines to a fraction of industry norms.

The approach has supported exports to the Middle East, Africa, Southeast Asia, and South America. The Mexico delivery extends this track record into a market where industrial buyers increasingly evaluate Chinese equipment on performance and service rather than price alone.

Mexico’s industrial base includes significant mining, petrochemical, and manufacturing activity. These sectors generate sludge, tailings, and granular waste that require safe, reliable transfer. The GNSP-10B’s dry conveying method—using air as the transport medium rather than water or oil—reduces secondary contamination and eliminates oil vapor emissions. This aligns with environmental compliance requirements that have tightened across Mexican industry in recent years.

The pump’s automatic operation also supports integration with PLC and HMI systems. While the GNSP-10B itself runs on pneumatic logic, it can be monitored and coordinated through plant control systems, enabling unmanned operation in remote or hazardous locations.

A single pump delivery is not a market transformation. But it does indicate that Mexican industrial buyers are actively evaluating non-traditional suppliers for material handling equipment. The GNSP-10B competes on specific technical merits: explosion-proof design, low maintenance requirements, dry conveying, and compact dimensions. For applications where electrical equipment is prohibited or impractical, the case for pneumatic vacuum transfer is straightforward.

GN pre-production inventory model addresses a common objection to overseas equipment—long lead times. By maintaining stock of complete units, the company reduces the gap between order and installation. Whether this advantage proves sustainable at larger scale depends on demand volume and inventory management discipline. For now, the Mexico delivery demonstrates that the model works for individual orders.

The broader question is whether pneumatic vacuum systems will gain share against electric alternatives in markets where both are viable. The GNSP-10B makes a credible argument for pneumatic technology in hazardous and high-wear applications. Its reception in Mexico suggests that argument is being heard.

GN Separation Will Attend WETEX 2026 in Dubai

GN Separation will exhibit at WETEX 2026, the 28th Water, Energy, Technology and Environment Exhibition, scheduled for October 20–22, 2026, at the Dubai World Trade Centre (DWTC). The company’s booth is located in Hall 4, Booth 4F07. WETEX is one of the Middle East’s largest and most established trade platforms for water, energy, and environmental technologies, organized under the umbrella of the Dubai Electricity and Water Authority (DEWA). For GN Separation, participation in this event represents a direct engagement with the region’s growing demand for efficient solid-liquid separation and sludge management solutions.

GN Separation specializes in the design and manufacture of centrifugal separation equipment and complete sludge treatment systems. The product portfolio includes decanter centrifuges, disc separators, solids vacuum pumps, vibrating screens, and screw press dewatering units. These machines serve industries ranging from municipal wastewater treatment and industrial effluent processing to oil sludge remediation and chemical production. At WETEX 2026, the company will present a selection of its core equipment, with technical staff available to discuss application-specific requirements.

One of the primary exhibits is the decanter centrifuge series, including the GNLW554 and GNLW364 models. The GNLW554 is a large-capacity unit suited to high-volume separation tasks, while the GNLW364 is a three-phase decanter capable of separating solids, oil, and water in a single continuous process. Three-phase separation is particularly relevant to oil sludge treatment, where the recovery of oil and the dewatering of solids must occur simultaneously. The disc separator, model Disc Separator 90, complements the decanter range by handling fine-particle separation duties where higher centrifugal force and tighter clarification are required.

For material transport within treatment systems, GN Separation offers the solids vacuum pump, including the GNSP-40 and GNSP-10 models. These pumps are designed to move high-viscosity, high-solid-content slurries that would otherwise clog conventional pumping equipment. By maintaining a stable flow of sludge and other dense media, the vacuum pumps reduce downtime and support continuous operation of the overall treatment train. The vibrating screen serves as a pre-treatment device, removing coarse debris before the slurry enters centrifuges or presses, thereby protecting downstream equipment and improving separation consistency.

The mini sludge screw press provides a compact dewatering option for smaller facilities or for sites where space is limited. It operates on the principle of volume reduction through mechanical compression, lowering the moisture content of sludge to facilitate transport and disposal. Together with the centrifuge and pump lines, these products form an integrated approach to solid-liquid separation, covering pre-treatment, conveyance, and final dewatering.

GN Separation’s equipment has been applied in several demanding industrial contexts. In ammonia-soda ash production, the company’s decanter centrifuges process white mud and salt mud without the need for prior sand separation, simplifying the flowsheet and improving overall material recovery. In oil sludge treatment, three-phase decanters enable the recovery of usable oil while producing drier solids for disposal. Municipal and industrial wastewater plants use the centrifuges for sludge thickening and dewatering, achieving consistent dryness and reducing the volume of waste requiring final disposal.

The company operates three manufacturing facilities in China with a total area of approximately 110,000 square meters. This production capacity supports both standard equipment lines and customized configurations. GN Separation has participated in international exhibitions across Asia, the Middle East, and Europe, including IE Expo China, Global Water Expo in Saudi Arabia, ASIA Water in Malaysia, and IFAT in Germany. These events have provided platforms for direct customer engagement and market development. The WETEX exhibition continues this pattern, placing GN Separation in direct contact with project developers, engineering firms, and utility operators active in the Gulf region.

WETEX 2026 will be held at the Dubai World Trade Centre, a venue that hosts thousands of exhibitors and visitors annually. The event includes technical seminars and networking sessions alongside the exhibition floor. GN Separation’s presence at Hall 4, Booth 4F07 offers attendees the opportunity to examine equipment specifications, discuss process design, and evaluate separation performance for specific applications. Additional information about the exhibition is available at https://www.wetex.ae/en.

For GN Separation, attending WETEX 2026 is a practical step in maintaining visibility within the Middle East’s environmental technology sector. The region’s investment in water reuse, industrial wastewater treatment, and waste minimization aligns with the company’s product capabilities. By presenting its centrifuges, pumps, and dewatering equipment at the DubaiWorld Trade Centre, GN Separation aims to support project requirements with equipment designed for continuous operation and consistent separation performance.

Decanter Centrifuges in Tailings Dewatering: The Role of Large-Bowl Design

Tailings management is one of the most pressing operational and environmental challenges in mining and mineral processing. As ore grades decline and regulatory pressure on tailings storage facilities increases, operators need dewatering equipment that can handle large volumes of fine-grained slurry continuously and reliably. Decanter centrifuges, particularly large-bowl models, have become a standard solution for this duty. This article examines why large-bowl decanter centrifuges are suited to tailings dewatering and what specific design features matter in practice.

Tailings are not a uniform material. They typically contain a wide particle size distribution, a significant fraction of fines below 20 microns, and variable mineralogy that affects settling behavior. Traditional separation methods—gravity settling, magnetic separation, and flotation—were not designed for the volumes and fine particle content that modern mining operations generate. Gravity thickeners can recover water but produce a underflow that still contains substantial moisture. Filter presses achieve high dryness but operate in batches and struggle with high-clay or slimy feeds. The result is that many operations face a bottleneck: they can move ore, but they cannot economically manage the waste stream.

A decanter centrifuge addresses this bottleneck by applying centrifugal force to accelerate settling. The unit consists of a rotating cylindrical-conical bowl and an internal scroll that rotates at a slightly different speed. Slurry enters through a feed tube, is accelerated to bowl speed, and the solid phase settles against the bowl wall under centrifugal force. The scroll conveys the settled solids toward the conical end for discharge, while clarified liquid exits at the cylindrical end. Because the process is continuous, the centrifuge can operate around the clock with minimal operator intervention.

The term “large bowl” refers to the diameter and length of the rotating assembly. A larger bowl diameter increases the settling area and the depth of the liquid pool, which improves separation of fine particles. A longer bowl increases the residence time of the slurry, allowing more complete settling. In tailings applications, where a substantial portion of solids may be in the 2–10 micron range, these two parameters directly determine performance.

Consider a representative large-bowl model with a 760 mm bowl diameter and a length of roughly 3,300 mm. The maximum rotational speed is approximately 2,650 rpm, generating a centrifugal force of about 3,000 G. At this G-level, particles that would take hours to settle under gravity settle in seconds. The theoretical cut point—the particle size at which separation efficiency is 50%—can reach 2 to 5 microns, depending on feed characteristics and operating parameters. This is a critical threshold: it means the centrifuge can capture fines that would otherwise report to the liquid phase and return to the process or require further treatment.

Throughput is equally important. A large-bowl unit can process up to 120 cubic meters per hour, which matches the output of a mid-to-large-scale mineral processing plant. The differential speed between bowl and scroll is adjustable, typically in the range of 5 to 28 rpm. This adjustability allows the operator to trade off between solids dryness and liquid clarity. A lower differential speed increases the solids residence time in the bowl, producing drier cake, while a higher differential speed improves liquid clarity by reducing the solids load in the pool.

Modern decanter centrifuges for tailings duty are equipped with variable frequency drives on both the main motor and the backdrive motor. This configuration allows independent control of bowl speed and differential speed, which is essential when feed properties change. For example, if the feed becomes finer or more viscous, the operator can reduce the differential speed to maintain solids dryness, or increase bowl speed to maintain liquid clarity. The ability to adjust these parameters in real time without shutting down the machine is a significant operational advantage over batch processes.

Power requirements reflect the scale of the machine. A large-bowl unit may use a 160 kW main motor and a 90 kW backdrive motor. While these figures appear high, the energy consumption per cubic meter of feed is often lower than that of filter presses when the entire cycle—including feed pumps, filter cloth replacement, and batch downtime—is accounted for.

Tailings slurries are abrasive. The presence of quartz, feldspar, and other hard minerals accelerates wear on the scroll flights and the bowl interior. For this reason, large-bowl decanters intended for mining service use wear-resistant materials. Duplex stainless steel 2304 is a common choice for the bowl and scroll body, offering a combination of corrosion resistance and mechanical strength. The scroll flights are often hard-surfaced or fitted with tungsten carbide tiles at the points of highest wear. Bearing selection also matters: SKF or equivalent bearings are standard to ensure reliability under continuous operation.

A decanter centrifuge is rarely installed as a standalone unit. In tailings dewatering, it is part of a system that includes feed pumps, flocculant dosing equipment, and conveyance for the dewatered cake. Modular containerized designs have become popular for remote or overseas projects. In this arrangement, the centrifuge is mounted on a steel frame within a shipping container, with the polymer dosing unit located below or adjacent. The container includes walkways, lighting, and ventilation, allowing the system to be commissioned quickly on site. This approach reduces civil works and shortens the timeline from delivery to operation.

Flocculant addition is often necessary when the tailings contain a high proportion of clay or ultrafine particles that resist centrifugal settling alone. The polymer bridges fine particles into larger flocs, which are then captured by the centrifuge. The feed system must introduce the flocculant with sufficient mixing energy to promote floc formation but without excessive shear that would break the flocs apart. Some designs use a gentle feed accelerator to minimize shear, which improves flocculation efficiency and reduces polymer consumption.

The primary outputs of tailings dewatering are a clarified liquid stream and a dewatered solids stream. The clarified liquid, often called centrate, can be returned to the process as wash water or make-up water. In many operations, this reduces fresh water intake by 70% or more, which is significant in arid regions or where water rights are constrained. The dewatered solids, typically in the range of 60–75% solids by weight depending on feed characteristics, can be conveyed to a dry stack. Dry stacking eliminates the need for a tailings dam, removing the risk of dam failure and the long-term liability of impoundment maintenance. It also allows progressive reclamation of the disposal area.

There is also a resource recovery angle. In tailings that contain residual metals or heavy minerals, the centrifuge concentrates these values in the solids stream. While the centrifuge is not a substitute for a full recovery circuit, it can improve the economics of downstream processing by reducing the volume of material that must be treated.

Selecting a large-bowl decanter for tailings duty requires attention to several factors beyond the machine itself. Feed characterization—particle size distribution, solids concentration, mineralogy, and rheology—should be conducted before sizing. Pilot testing is advisable when the tailings are unfamiliar or when the target dryness is aggressive. The control system should allow for automatic adjustment of differential speed based on torque or solids load, which reduces operator workload and protects the machine from overload. Finally, maintenance access should be considered at the design stage: bowl removal and scroll inspection require space and lifting equipment.

Large-bowl decanter centrifuges have become a practical and widely adopted solution for tailings dewatering. Their continuous operation, high throughput, and ability to capture fine particles make them suitable for the volumes and material characteristics typical of modern mining operations. When integrated with flocculant dosing and containerized packaging, they offer a deployable system that reduces water consumption, eliminates tailings dams, and lowers long-term environmental risk. For operations facing tightening regulations and rising water costs, the large-bowl decanter is not merely an option but a core component of the tailings management strategy.

GN Trenchless Mud Recycling Systems for Overseas Engineering Company

GN Solids Control, officially known as Hebei GN Solids Control Co., Ltd., has established a consistent export record for its trenchless mud recycling systems and TBM slurry separation equipment. The company supplies horizontal directional drilling (HDD) mud purification systems and tunnel boring machine (TBM) slurry treatment plants to overseas engineering contractors across Europe, the Middle East, Africa, and Asia. This article outlines the product scope, technical configuration, and market applications of these systems.

GN Solids Control is a national high-tech enterprise and has been recognized as a “Little Giant” enterprise by China’s Ministry of Industry and Information Technology. The company operates two manufacturing bases in China, with its headquarters in Langfang, Hebei Province, and a sales center in Beijing. Its U.S. brand, GN Solids America, supports North American and international customers. GN was the first Chinese manufacturer to develop and export mud cuttings dryers, and it maintains a global service network covering major trenchless construction markets.

For horizontal directional drilling projects, GN manufactures a range of mud recycling systems under its K, B, and C series. The K series provides economical configurations for basic mud purification. The B series offers higher integration and automation for mid-to-high-end projects. The C series is customized for specific overseas standards, including European CE and environmental requirements. Recent exports to Europe include two GNMS-400C units and one GNMS-200C unit, delivered to a trenchless engineering contractor.

Typical system models include the GNMS-200B, GNMS-400B, GNMS-500GPM, GNMS-600B, and GNMS-800B. Processing capacities range from 150 GPM (approximately 30 m³/h) to 1500 GPM (approximately 360 m³/h), with common configurations at 350 GPM, 500 GPM, and 1000 GPM. A standard HDD mud recycling system integrates a shale shaker for coarse solids removal, a desander and desilter cyclones for fine particle separation, and a decanter centrifuge for high-precision solid-liquid separation. Optional equipment includes high-G drying shakers and screw conveyors for cuttings dryness. The system enables closed-loop mud circulation, reducing fresh mud consumption and waste discharge.

In Egypt, GN has maintained a market presence since 2011. A long-term trenchless contractor recently purchased a Vermeer 400-ton drilling rig for an oil pipeline project and selected a GNMS-500GPM mud purification system to match the rig’s capacity. This repeat order reflects sustained customer confidence in GN’s equipment and after-sales support. In the Middle East, an HDD mud recycling system passed factory acceptance testing before shipment to a regional contractor. In Asia, GN supplied two GNMS-1500GPM slurry separation stations and one GNMS-200 mud recycling system for a large-scale trenchless project.

For tunnel boring machine projects, GN provides mud-water separation plants designed to handle large volumes of slurry with high solid content. The GNMS-1500GPM slurry separation station is a representative model, capable of processing up to 360 m³/h. These systems combine coarse screening, cyclone classification, and centrifuge dewatering to separate excavated solids from the slurry, allowing the cleaned fluid to be recirculated back to the TBM. The separated solids are discharged in a dry, handleable form, reducing transportation and disposal costs. This configuration is applicable to both slurry shield TBM and mix shield TBM operations

GN’s mud recycling and slurry separation systems share several design features that support overseas deployment. The equipment is modular and compact, facilitating containerized transport and rapid on-site assembly. Components are selected for compatibility with international electrical and safety standards. The systems accommodate varying mud compositions and flow rates, allowing configuration changes without major structural modification. GN’s in-house manufacturing covers key components including shale shakers, cyclones, and decanter centrifuges, which supports consistent quality control and spare parts availability.

For overseas engineering contractors, the primary value of these systems lies in cost reduction and regulatory compliance. By recovering and reusing drilling fluid, contractors decrease the purchase volume of fresh mud materials and reduce the volume of waste mud requiring disposal. This directly lowers project operating costs and helps meet environmental regulations in jurisdictions with strict discharge controls. The dried cuttings output further reduces waste handling and transport expenses.

GN provides selection consultation, installation guidance, commissioning support, and spare parts supply through its international service network. In established markets such as Egypt, long-term service relationships have contributed to repeat orders and referrals. For new customers, GN offers system customization based on drilling rig specifications, expected mud flow rates, and site conditions. Documentation and technical support are available in English and other languages as required.

GN Solids Control’s HDD mud recycling systems and TBM slurry separation systems have been delivered to engineering contractors in Europe, Africa, the Middle East, and Asia. The product range covers processing capacities from 150 GPM to 1500 GPM, with configurations adapted to different project scales and regulatory environments. The combination of modular design, in-house component manufacturing, and international service support positions GN as a practical equipment supplier for overseas trenchless and tunneling contractors seeking mud treatment solutions.

Four Sets Drililng Mud Tank Cleaning Waste Water Treatment Unit for Africa

In September 2026, GN Solids Control completed the shipment of four complete drilling mud tank washing wastewater treatment systems to an African client. This order represents a significant advancement in the company’s ongoing expansion within the African market, where demand for environmentally compliant drilling waste management solutions has grown substantially in recent years.

The four systems are designed to address a specific operational challenge faced by drilling contractors across the continent: the safe and efficient treatment of wastewater generated during the routine cleaning of mud tanks. Traditional methods of disposing of this wastewater often involve open pits or uncontrolled discharge, both of which carry significant environmental and regulatory risks. The systems supplied by GN Solids Control provide a contained, mechanized alternative that treats the water on-site, allowing for reuse in future drilling operations or safe disposal.

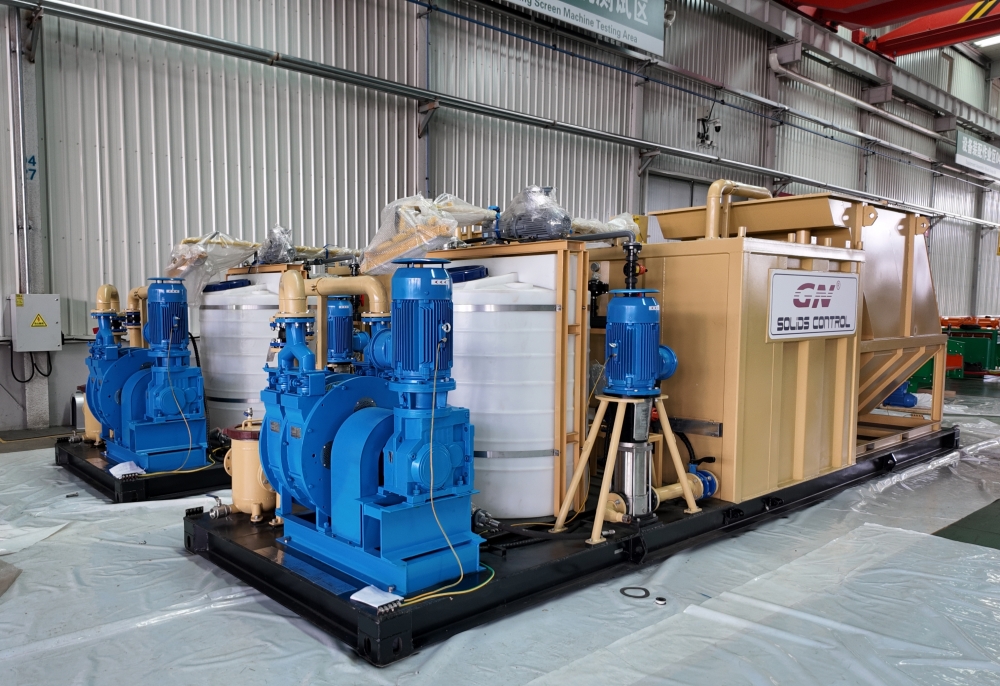
Each of the four systems is built around a core processing train that begins with solids separation. Wastewater entering the system first passes through a shale shaker equipped with composite framework screens, which removes large particles and debris that could damage downstream equipment. Following this primary separation stage, the water moves through a series of hydrocyclones—desanders and desilters—that extract finer sand and silt particles. The final mechanical separation step utilizes a decanter centrifuge, which spins at high speed to remove ultra-fine suspended solids, producing a clarified liquid stream.

The chemical treatment stage complements the mechanical separation. Each system includes an automatic polymer dosing unit with three tanks, allowing operators to mix and inject flocculants and coagulants at precise concentrations. These chemicals cause suspended particles to aggregate into larger flocs, which the centrifuge can then remove more effectively. The dosing system supports both automatic and manual operation modes, giving the client flexibility depending on the specific wastewater characteristics encountered at each site.

Tank cleaning functionality is integrated into the system design. Each unit is equipped with rotating mud guns that generate high-pressure fluid streams capable of scouring tank walls and removing accumulated residues. This feature addresses a common pain point for drilling operators in Africa, where manual tank cleaning is both labor-intensive and hazardous. By automating the cleaning process and routing the resulting wastewater directly into the treatment system, the equipment reduces downtime and minimizes worker exposure to potentially harmful substances.

The systems are configured for rapid deployment in remote locations. They are mounted on standard skids with fork-lift pockets and lifting lugs, enabling easy transport via flatbed truck or container. On-site installation requires only basic utility connections: power, water supply, and a discharge point for the treated effluent. This plug-and-play design is particularly valuable for African drilling operations, many of which are situated in areas with limited infrastructure and where construction of permanent treatment facilities would be cost-prohibitive.

The African client that placed this order operates multiple drilling rigs across several countries and has previously purchased solids control equipment from GN Solids Control. Their decision to acquire four complete wastewater treatment systems in a single order reflects both their satisfaction with prior purchases and their need to standardize waste management practices across their various sites. The client’s technical team reviewed and approved the system design, which incorporates several modifications based on feedback from earlier projects in the region. These include reinforced electrical cabinets to withstand dusty environments, oversized screens to handle high solids loadings, and simplified control interfaces that reduce the training burden for local operators.

This shipment contributes to a broader trend of African drilling contractors investing in modern environmental protection equipment. Regulatory frameworks across the continent are becoming more stringent regarding drilling waste management, and operators are recognizing that proactive investment in treatment technology is more cost-effective than facing fines, cleanup orders, or project suspensions. The four systems supplied by GN Solids Control will enable this client to maintain compliance with national regulations while also improving their operational efficiency through reduced water consumption and faster tank turnaround times.

The transaction also underscores the growing capability of Chinese manufacturers to deliver sophisticated environmental engineering solutions to international markets. GN Solids Control has invested heavily in research and development, resulting in equipment that matches or exceeds the performance of Western competitors at a more accessible price point. The company’s ability to customize systems for specific regional conditions, combined with reliable after-sales support, has made them a preferred supplier for many African drilling contractors.

With this delivery, GN Solids Control continues to strengthen its position as a leading provider of drilling waste management technology in Africa. The successful commissioning of these four systems will likely generate additional orders from other operators facing similar wastewater treatment challenges across the continent.

GN Solids Vauum Pump and Decanter Centrifuge for Middle East Client

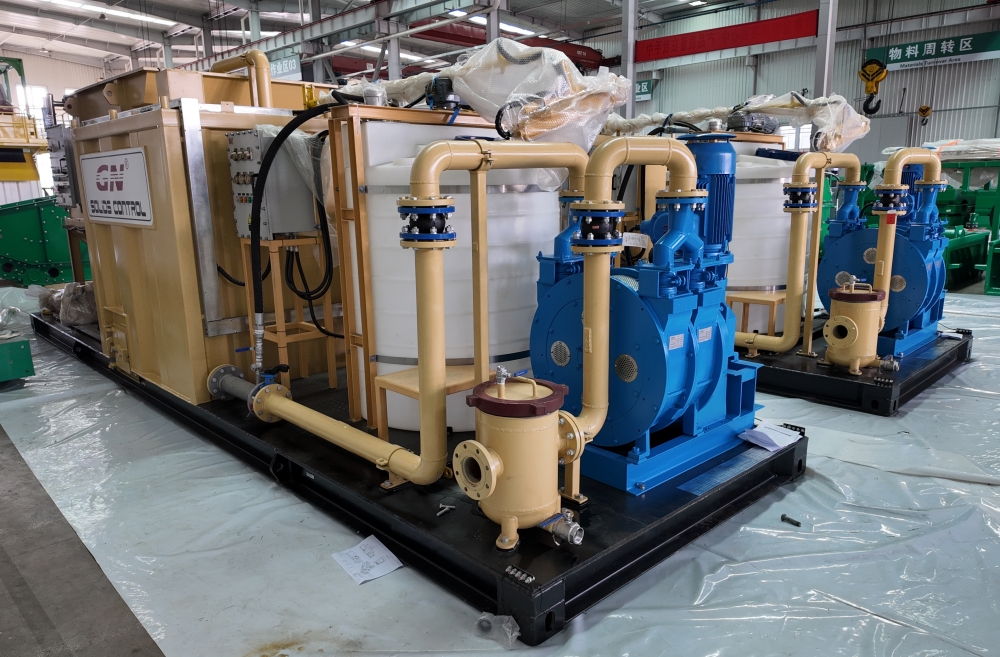
GN Solids Control recently completed a significant shipment of solid vacuum pumps and decanter centrifuges to a Middle Eastern oilfield services company. The order included three solid vacuum pumps, one mud cleaner, and one decanter centrifuge, marking another milestone in the company’s expanding presence in the region. This transaction was not an isolated event but part of a broader pattern of repeat business from established clients in the Middle East, where GN has been supplying solid-liquid separation equipment for years.

The Middle East presents a demanding environment for drilling operations. High temperatures, abrasive materials, and stringent environmental regulations require equipment that can handle tough conditions while maintaining safety and efficiency. Traditional separation methods often fall short when dealing with high-density materials such as tank bottom sludge, drilling cuttings, and refinery waste. This is where GN’s equipment demonstrates its value. The solid vacuum pump, for instance, uses a purely pneumatic drive system with a Venturi mechanism that generates vacuum levels up to 25 inches of mercury. Because all valves and control components are air-driven, there is no risk of electrical sparks, making the pump suitable for explosive atmospheres commonly found in oil and gas sites. It is specifically designed to transport thick, high-density slurries and solid-liquid mixtures that would clog or damage conventional pumps.

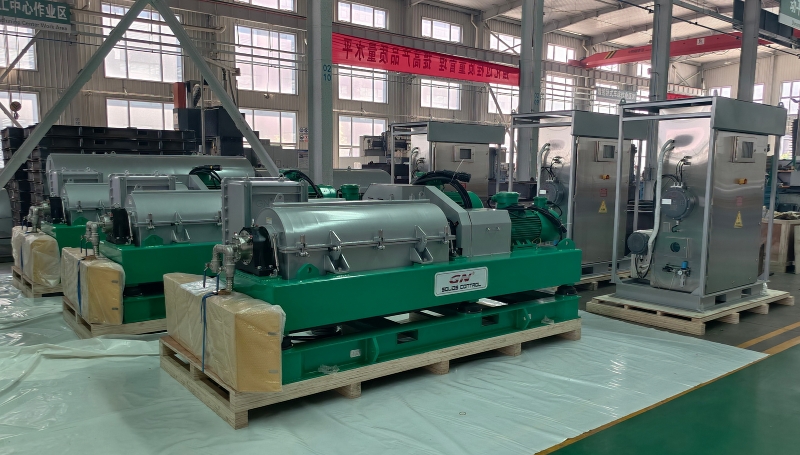
The decanter centrifuges shipped in this batch include both variable-frequency drive models and fully hydraulic versions. The GNLW554ET-VFD, a 22-inch unit, is capable of separating solid particles down to 2-5 microns, making it suitable for large-scale drilling fluid purification and waste volume reduction. The fully hydraulic centrifuges, developed in cooperation with Swiss brands Viscotherm and ROTODIFF, underwent extensive factory testing before shipment. These units offer smooth speed adjustment and reliable heavy-load starting, which are critical in extreme operating conditions. The inclusion of three-phase decanter centrifuges, such as the GNLW364 model, further expands the application range to oil-water-solid separation in oily sludge treatment.

Beyond the primary equipment, the shipment also included customized screw conveyors designed specifically for the customer’s site layout. These conveyors transfer separated solids continuously and are built with wear-resistant spiral blades to extend service life. The removable covers and steel grating options improve both safety and maintenance convenience. This attention to auxiliary components reflects GN’s approach of delivering complete systems rather than standalone machines. The company also supplies mud cleaners, vertical cuttings dryers, and centrifugal pumps compatible with major international brands, allowing clients to standardize their spare parts inventory and reduce operational costs.

The repeat orders from Middle Eastern clients did not happen by chance. GN has invested considerable effort in understanding regional requirements, including explosion-proof standards, material handling characteristics, and environmental compliance. The company’s ability to customize equipment based on specific project needs has been a decisive factor. For example, the 12 drilling cuttings screw conveyors in this order were tailored to the customer’s installation requirements, demonstrating a level of flexibility that large multinational competitors often struggle to match. Additionally, all equipment undergoes rigorous factory testing before delivery, ensuring that units arrive on-site ready for installation and operation. This quality control process minimizes downtime and gives clients confidence in the reliability of the products.

From a broader perspective, this shipment illustrates a shift in how Chinese manufacturers compete internationally. The focus has moved from price advantage to a combination of technology, customization, and after-sales support. GN’s progress in the Middle East is a case in point: by offering equipment that matches or exceeds the performance of established Western brands while providing tailored solutions and responsive service, the company has built lasting relationships with clients who value long-term reliability over initial cost savings. The fact that many orders come from repeat customers indicates that the equipment performs well in real-world conditions, which is the strongest endorsement any industrial supplier can receive.

Looking ahead, the demand for efficient solid-liquid separation and waste management in the Middle East is expected to grow as environmental regulations tighten and operators seek to reduce their ecological footprint. GN’s continued investment in research and development, particularly in areas like oily sludge treatment and three-phase separation, positions the company well to capture additional market share. The successful delivery of this batch of solid vacuum pumps and decanter centrifuges serves as a practical demonstration of the company’s capabilities and reinforces its reputation as a reliable partner for complex separation challenges in the region.

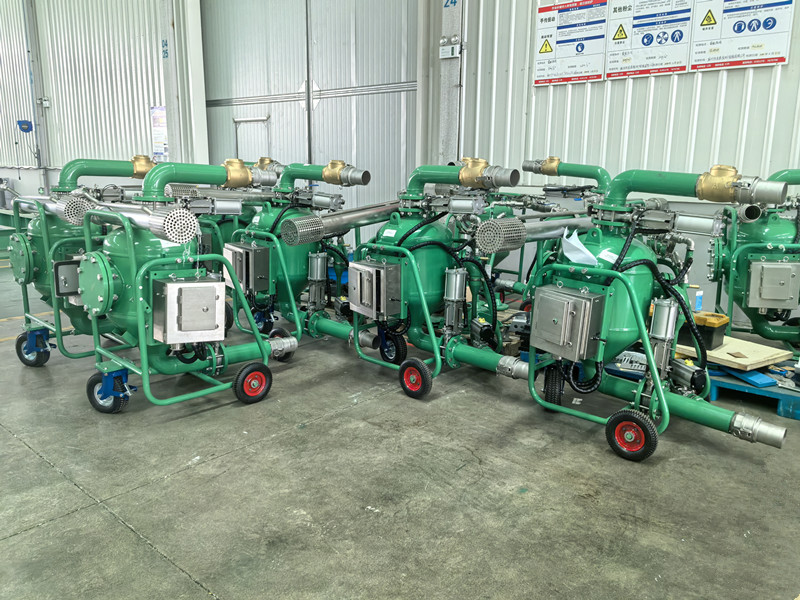
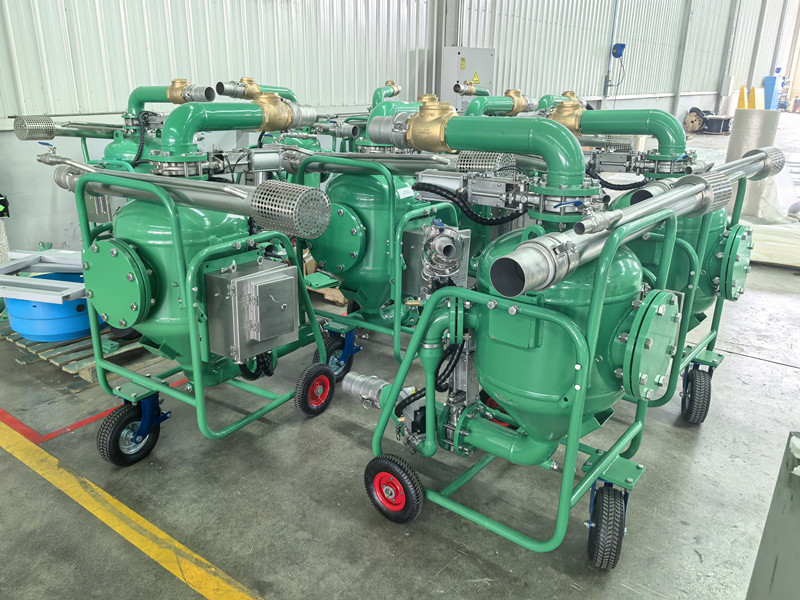
A Batch of GNSP20B Solids Vacuum Pump Ready for Shipment

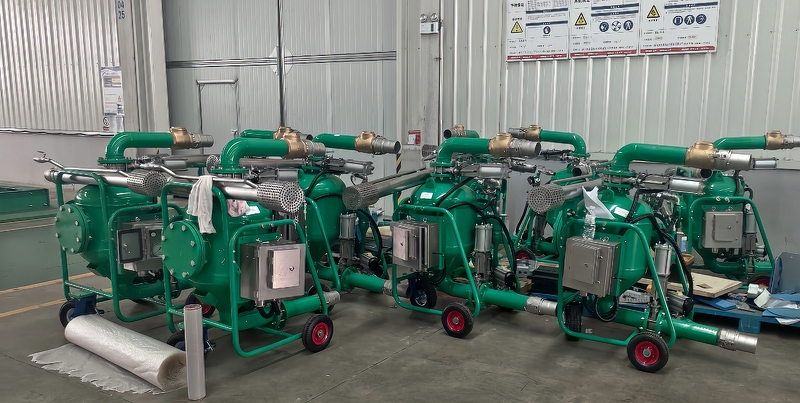
A batch of solid vacuum pumps has completed final testing and is now cleared for shipment. This delivery represents the culmination of a rigorous quality assurance process, not a routine warehouse dispatch. Every unit in this batch underwent a 100% performance inspection using a computer-controlled testing system that measures and records the complete performance curve of each pump.

The testing protocol for this batch followed established industrial standards. Each vacuum pump was connected to a test rig equipped with calibrated vacuum measurement devices that maintain NIST traceability. This ensures the accuracy of all recorded data and provides verifiable proof that each unit meets its specified performance parameters. The test data for every pump has been archived and is available for customer review, offering full transparency into the quality control process.

The performance verification focused on several key operational metrics. Suction capacity was measured to confirm each unit achieves its rated vacuum level within the specified time frame. Power consumption was monitored to ensure energy efficiency falls within acceptable tolerances. Vibration and noise levels were also assessed, as these factors directly impact the operational lifespan of the pump and its suitability for various installation environments.

The pumps in this batch are designed for handling dry, solid particulate matter in industrial applications. Their construction features wear-resistant components that withstand abrasive materials without compromising performance. The internal rotor and vane geometry has been optimized to maintain consistent suction force even when processing fine powders or granular solids. This design makes them suitable for pneumatic conveying systems, dust collection setups, and material handling processes across multiple industries.

Each unit underwent a burn-in period during testing, running continuously for a set duration to identify any potential early-life failures. This accelerated aging process helps ensure that the pumps delivered to customers have already demonstrated operational stability beyond initial startup. The burn-in phase also allows technicians to verify that all seals maintain integrity under sustained vacuum conditions, preventing leaks that could reduce efficiency or allow contamination.

The shipment preparation follows a structured protocol designed to protect the equipment during transit. Each vacuum pump is individually sealed to prevent moisture ingress and contamination. The pumps are then secured in custom packaging that isolates them from vibration and impact forces encountered during freight handling. For this batch, the packaging configuration separates the pump body from any auxiliary components, reducing overall shipment volume and allowing more efficient use of cargo space.

The destination for this batch includes multiple industrial facilities that have integrated these pumps into their production lines. The confirmed orders reflect the growing demand for reliable solids-handling vacuum equipment in sectors such as cement processing, food powder handling, and chemical manufacturing. The delivery schedule has been coordinated with each customer’s installation timeline, allowing them to plan their commissioning activities with certainty.

This shipment also represents the manufacturer’s commitment to maintaining adequate inventory levels for their distribution network. By completing the full testing cycle before dispatch, the company ensures that their partners receive equipment that is ready for immediate installation without requiring additional on-site verification. This practice reduces the customer’s incoming inspection burden and accelerates their time-to-production.

The completion of this testing and dispatch cycle reinforces the manufacturer’s position as a dependable supplier of industrial vacuum technology. The documented performance data accompanying this shipment provides customers with a baseline for ongoing equipment monitoring and maintenance planning. This information also supports warranty claims and future service decisions, creating a complete equipment lifecycle record from factory acceptance to field operation.

GN Solids 14000BBL Rapid Liquid Mud Plant for Drililng Fluids Company

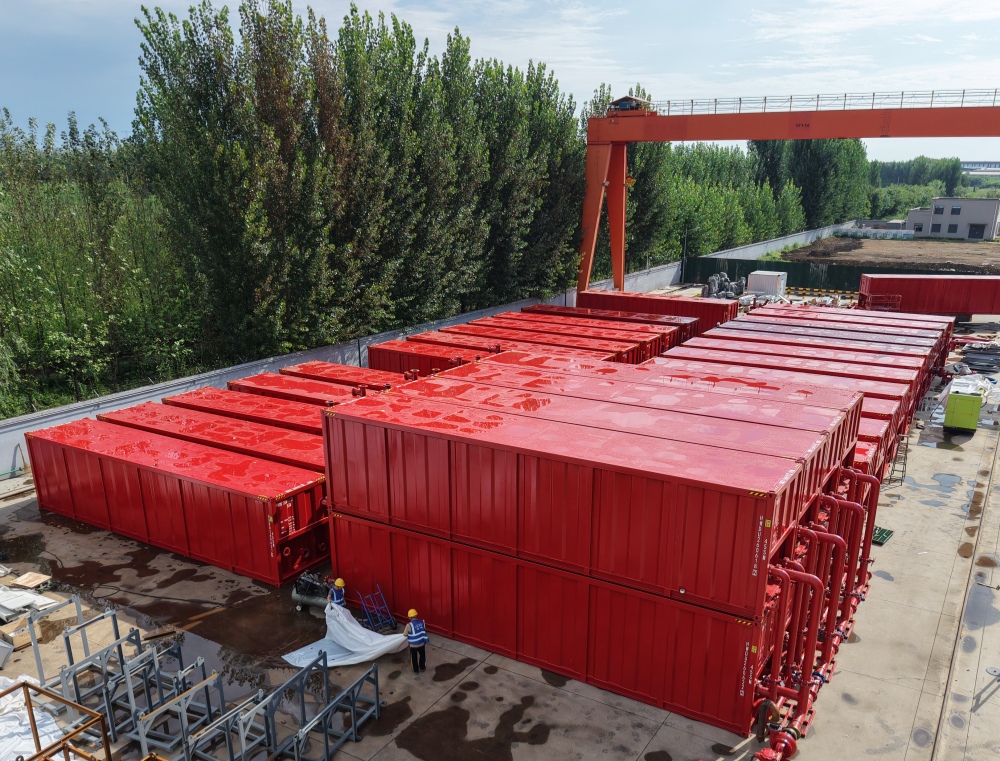
On August 28, 2026, GN Solids Control, a leading manufacturer of drilling fluid control equipment based in Hebei Province, China, announced the successful delivery of a 14,000-barrel rapid-deployment mud station to a major drilling fluids company. This order marks a significant milestone for the company, reinforcing its position as a key international supplier of high-capacity, modular mud systems. The 14,000BBL mud station is not a single tank but a complete system engineered for large-scale drilling operations, offering a substantial liquid storage and management capacity tailored to meet the demands of complex drilling projects.

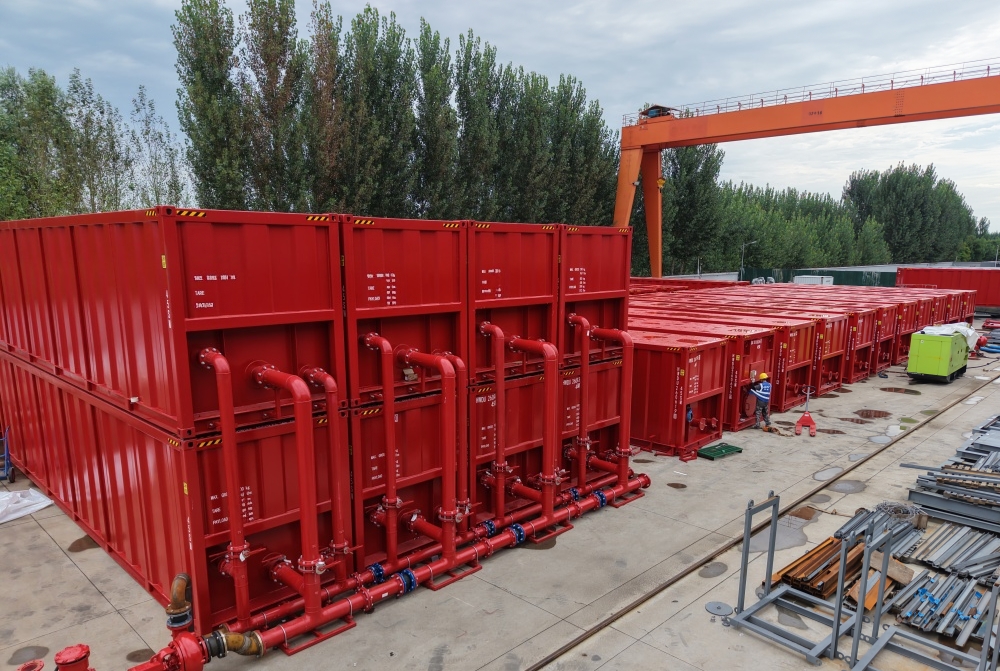
The core of this system lies in its modular design and adherence to international standards. The entire mud station is constructed around a series of 40-foot high-cube containers, each with a capacity of 440 barrels. This standardized unit approach provides exceptional logistical flexibility. The containers are designed and built to meet the rigorous requirements of the API-650 standard, ensuring structural integrity, safety, and reliability for petroleum and chemical storage. Furthermore, each container holds a CSC (Container Safety Convention) certification, which is critical for international shipping. This certification allows the containers to be transported seamlessly via standard container vessels, trucks, and rail, dramatically simplifying the logistics of mobilizing a large-capacity mud system to remote or overseas drilling sites.

A key design feature of this 14,000BBL mud station is its capability for two-layer stacking. This intelligent configuration allows operators to maximize the use of available space, a crucial advantage on congested drill sites or in areas with a limited footprint. By stacking the containers, the total ground area required for the mud station is significantly reduced, while still providing the full 14,000 barrels of storage and processing volume. This design also facilitates a more centralized and efficient layout for piping, cabling, and operational control, contributing to improved safety and workflow on location.

For the client, a specialized drilling fluids company, this rapid-deployment mud station offers a turnkey solution. It is not merely a set of storage tanks but an integrated system designed for efficient mud management. The station is equipped to handle the complete lifecycle of drilling fluid, including storage, mixing, and conditioning. The integration of GN Solids Control’s own high-performance equipment, such as mud mixers, mud guns, and centrifugal pumps, ensures that the system operates as a cohesive and efficient unit. The “rapid-deployment” aspect is a direct response to the industry’s need for speed and efficiency; once the containers arrive on site, setup and commissioning can be completed in a fraction of the time required for traditional, site-built mud systems.


This sale is a strong indicator of the growing global demand for modular and movable drilling support equipment. Oil and gas operators are continuously seeking ways to reduce capital expenditure and operational downtime. The ability to relocate a complete mud station quickly to a new well pad or a different project entirely represents a significant economic advantage. For drilling fluid companies, this flexibility means they can better serve their clients by providing high-quality mud services with faster turnaround times and reduced logistical complexity.

GN Solids Control’s success in securing this order is built on a foundation of proven engineering and manufacturing expertise. As the first Chinese manufacturer of solid control equipment to receive the American Petroleum Institute (API) management certification, the company has long demonstrated its commitment to quality and international standards. This order further validates that commitment, showcasing the company’s capability to deliver complex, large-scale projects that meet the stringent specifications of professional drilling fluid service companies. The completion and delivery of this 14,000BBL rapid-deployment mud station solidifies GN Solids Control’s reputation as a reliable partner for high-capacity, internationally compliant, and operationally efficient drilling fluid management solutions.